

NOTE:
Questions? Call 901-553-9847


XCMG XE210 - XE300 Series Excavator Cylinder Head Reman - Workhorse (6.7L)

Starting at:
- $2,350.00
- $2,350.00
- Unit price
- per
- Fully Remanufactured - New Critical Components
- Better Than Stock - Eliminates Several Factory Flaws
- Best Warranty In The Business
Don't guess on your engine.
Call us today to lock in your specs and get an exact shipping estimate.
Vendor:
Choate Performance
SKU:
CEPXCMGWHR
Barcode:
693793318904
Availability:
In stock
Product type:
Cylinder Head


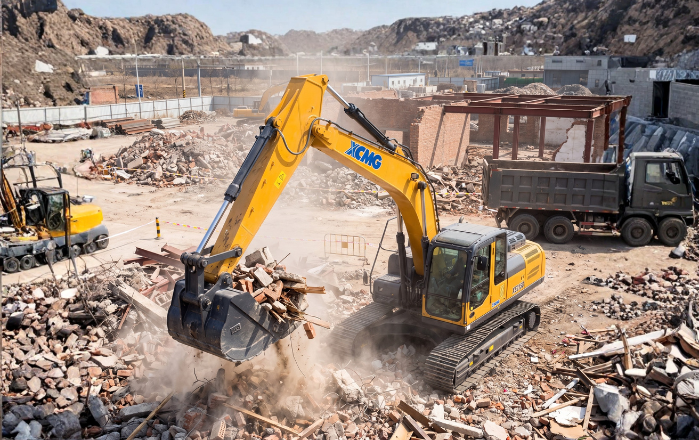
Heavy-Duty Ready
Day-in, day-out operation requires a cylinder head that can handle relentless thermal cycles and severe internal pressures. Our Workhorse tier XCMG 6.7L cylinder heads take all the precision engineering of our Daily Driver and add a critical structural upgrade designed for continuous operations.
The Workhorse Advantage: Precision Deck O-Rings

Improved Valvetrain Geometry

Precision Resurfacing

Blow-Proof Threaded Plugs

Testing and Quality Control

Full Description
Direct Fit For XCMG Excavator Models: XE210U, XE210UCA, XE215U, XE225U, XE235UCR, XE245UCR, XE250U, XE300U, and XE215D
Maximize machine availability and protect your equipment against head gasket failures during punishing excavation operations. The Workhorse tier cylinder head for XCMG XE210 through XE300 series crawler excavators is engineered specifically to handle continuous heavy-duty digging cycles, severe thermal loads, and relentless hydraulic system pressure. Assembled using a renewed, pressure-tested OEM core combined with brand-new, premium internal components, this cylinder head integrates heavy-duty structural upgrades to handle elevated cylinder pressures and eliminate common field failures on the job site.
Upgrades Over the Daily Driver: Precision O-Rings
Heavy excavation and demolition work generate intense internal heat and rapid thermal cycles, which are the leading causes of head gasket blowouts in production machinery. The Workhorse model eliminates this vulnerability by featuring precision-cut O-rings machined directly into the deck surface. This mechanical modification locks the head gasket securely in place, drastically improving sealing under high cylinder pressures and severe operating temperatures to guarantee zero combustion leaks and prevent costly operational downtime.
Components and Parts
-
Remanufactured Casting: Built from a high-quality OEM core casting that has passed rigorous diagnostic testing and is machined to like-new industrial specifications.
Key Features and Heavy-Duty Fixes
This industrial-grade head features critical durability updates, backed by an intense inspection protocol to guarantee every commercial specification is met.
-
40 PSI Pressure Testing: Following all machining work, every cylinder head is pressure-tested at 40 PSI to confirm zero leaks and ensure complete casting integrity before it ever reaches your machine.
-
Blow-Proof Plugs: Threaded, blow-proof plugs are installed in the top of the head for superior leak prevention, replacing standard factory pressed-in plugs that are prone to failure during severe thermal cycles.
-
Final Quality Control: The head undergoes an extensive final cleaning and strict inspection process. A detailed sign-off sheet is generated, measuring and recording critical specifications using a profilometer, including:
-
Valve Recessions
-
Stem Heights
-
Installed Spring Heights
-
Spring Pressures
-
Keeper and Lock Positions
-
Roughness Average (RA) Surface Finish
-
Recording This rigorous validation process ensures you receive a cylinder head that is significantly improved over the original factory design and ready for years of demanding excavator operation.
Precision Machining Process
Choate Engineering Performance has incorporated critical modifications to address common failure points of factory 6.7L cylinder heads, drastically improving field reliability:
-
Optimal Sealing Surface: The deck is resurfaced to meet or exceed OEM specifications for Roughness Average (Ra), maximizing the sealing surface performance for the head gasket under high-pressure common rail injection loads.
-
Valve Train Geometry Alteration: We custom blueprint the 6.7L head to alter valve height and valve recession, achieving maximum durability for high-cycle excavator applications.
-
Lifter and Crosshead Longevity Fix: Valve stem heights are precisely altered to optimize geometry and remove excessive preload on the hydraulic lifter. This crucial modification decreases wear and significantly extends the life of the lifters, crossheads, and camshaft under constant high hydraulic demands.
-
Optimized Flow and Sealing: Valve seats are cut with a precise three-angle profile to optimize combustion efficiency and ensure a perfect seal.
-
Valve Prep: Valves are reground and margins are meticulously inspected to guarantee proper sealing against the new seats.
-
All-New Wear Components: New valve stem seals, valve seats, valve guides, and injector cups are installed across the entire assembly.
Meticulous Cleaning and Prep Process
Our commitment to quality begins before machining, with an intensive cleaning and stress-relieving process to ensure a flawless starting point:
-
Rigorous Inspection (MPI): Each core is subjected to Magnetic Particle Inspection (MPI) to thoroughly check for any cracks or subsurface imperfections common in high-hour castings.
-
Thermal Stress Relieving: The head undergoes a stress-relieving process in a specialized furnace to bake away residual industrial oils and grease by turning them into ash.
-
Material Relaxation: The head is shot-blasted to strip rust and scale, a crucial step that relaxes the cast iron before any precision machining begins.
-
Thread Prep: All broken factory bolts and studs are professionally removed to ensure threads are clean, chased, and ready for a seamless installation.
Warranty
Choate Engineering Industrial engines are covered up 2 year / 2,000 hours, with some limitations.
We also require our customers to follow proper maintenance procedures, replace critical components during installation, and more.
As consideration for the above warranties, the buyer agrees they will take no action, statement, characterization, or implication regarding Choate Engineering Performance that may in any manner be interpreted as disparaging to Choate Engineering Performance or the reputation of Choate Engineering Performance. Any violation of this is a material breach, entitling Choate Engineering Performance to void any warranty.
Freight/Shipping Charges
CHOATE ENGINEERING PERFORMANCE SHALL NOT BE RESPONSIBLE, NOR SHALL IT PAY ANY FREIGHT/SHIPPING CHARGES.
- All freight and shipping charges are the sole responsibility of the customer, including any customs fees or brokerage fees.
- Any shipments Choate Engineering Performance arranges for the customer include insurance.
- In the event the purchased unit is damaged during transportation to or from Choate Engineering Performance, Choate Engineering Performance shall not be responsible for any costs associated with such damage.
- The repair of such damage is not included under the Limited Warranty; should transportation damage skew the results of the diagnosis such that the findings are that the defect is not covered under the Limited Warranty, Choate Engineering Performance shall incur no liability or responsibility whatsoever.
What Makes Choate Engineering Performance Different?
We deck our blocks. Why we use blueprint boring. We use torque plate honing. Watch our videos to learn why these differences are important.
- Choosing a selection results in a full page refresh.